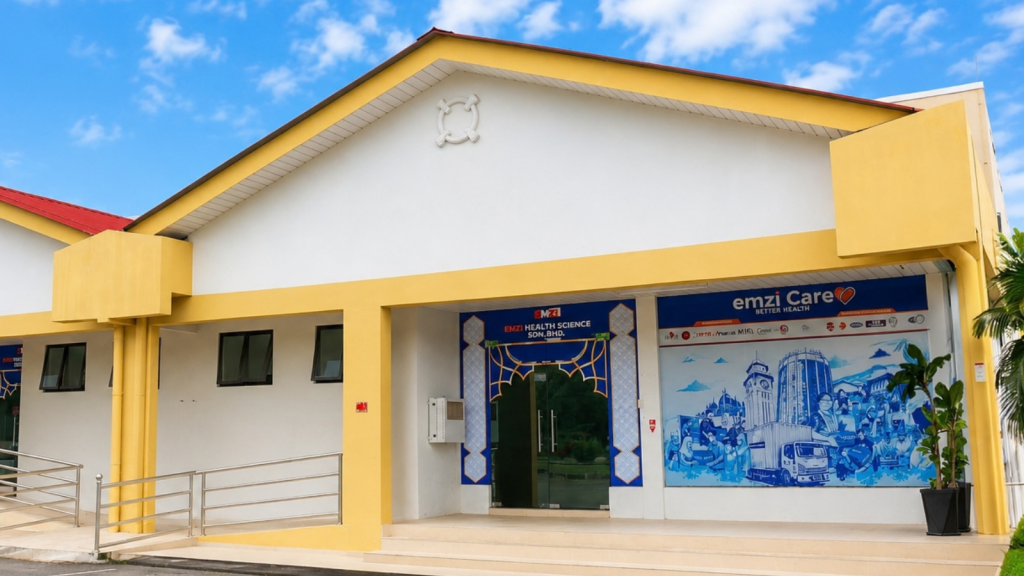
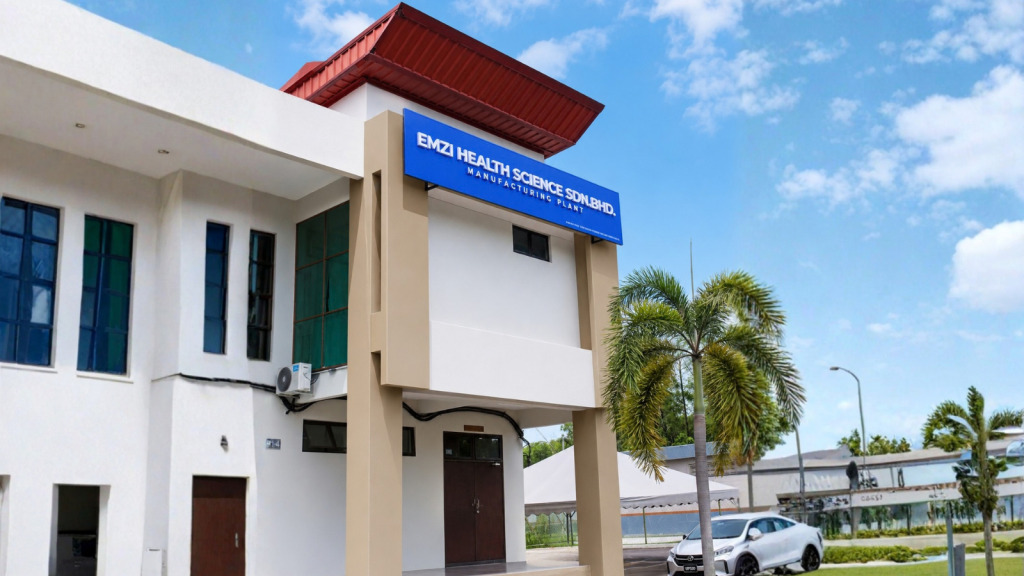
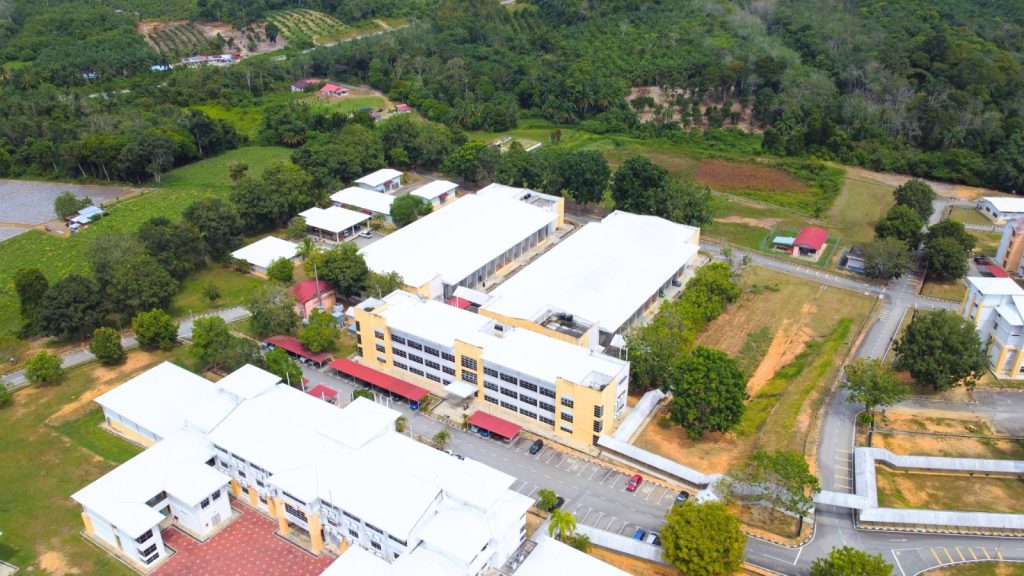
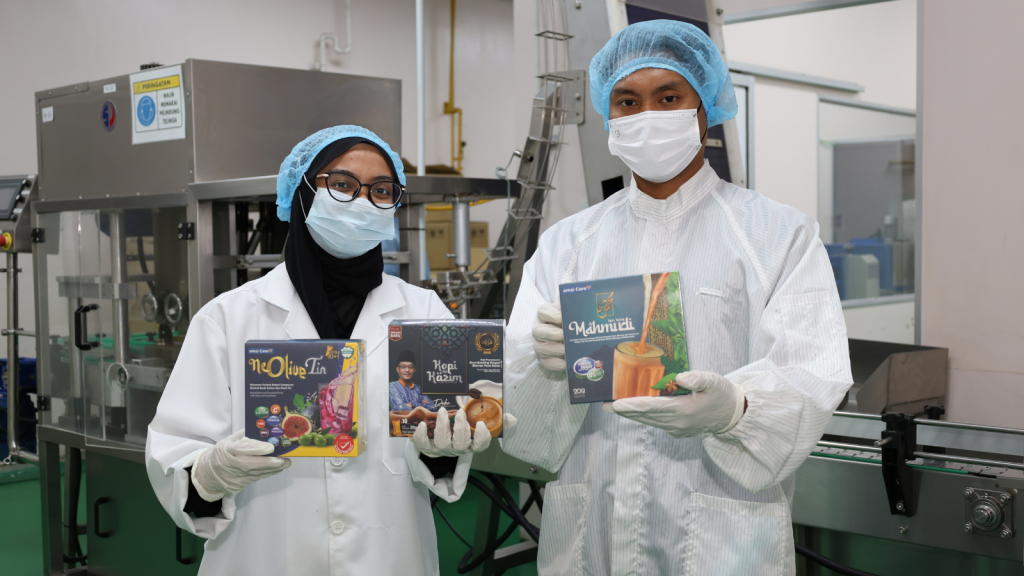
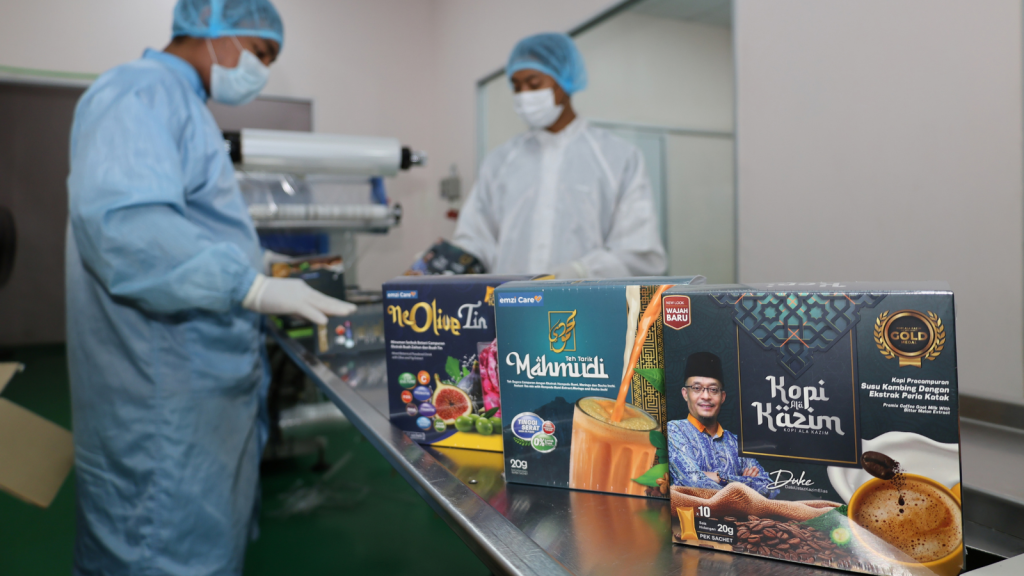
Established in 2020 and based at Kedah Halal Park, EMZI Health Science Sdn. Bhd. is a subsidiary of EMZI Holding Sdn. Bhd. operating a modern manufacturing facility that delivers high-quality health and wellness products through efficient, scalable and internationally aligned processes.
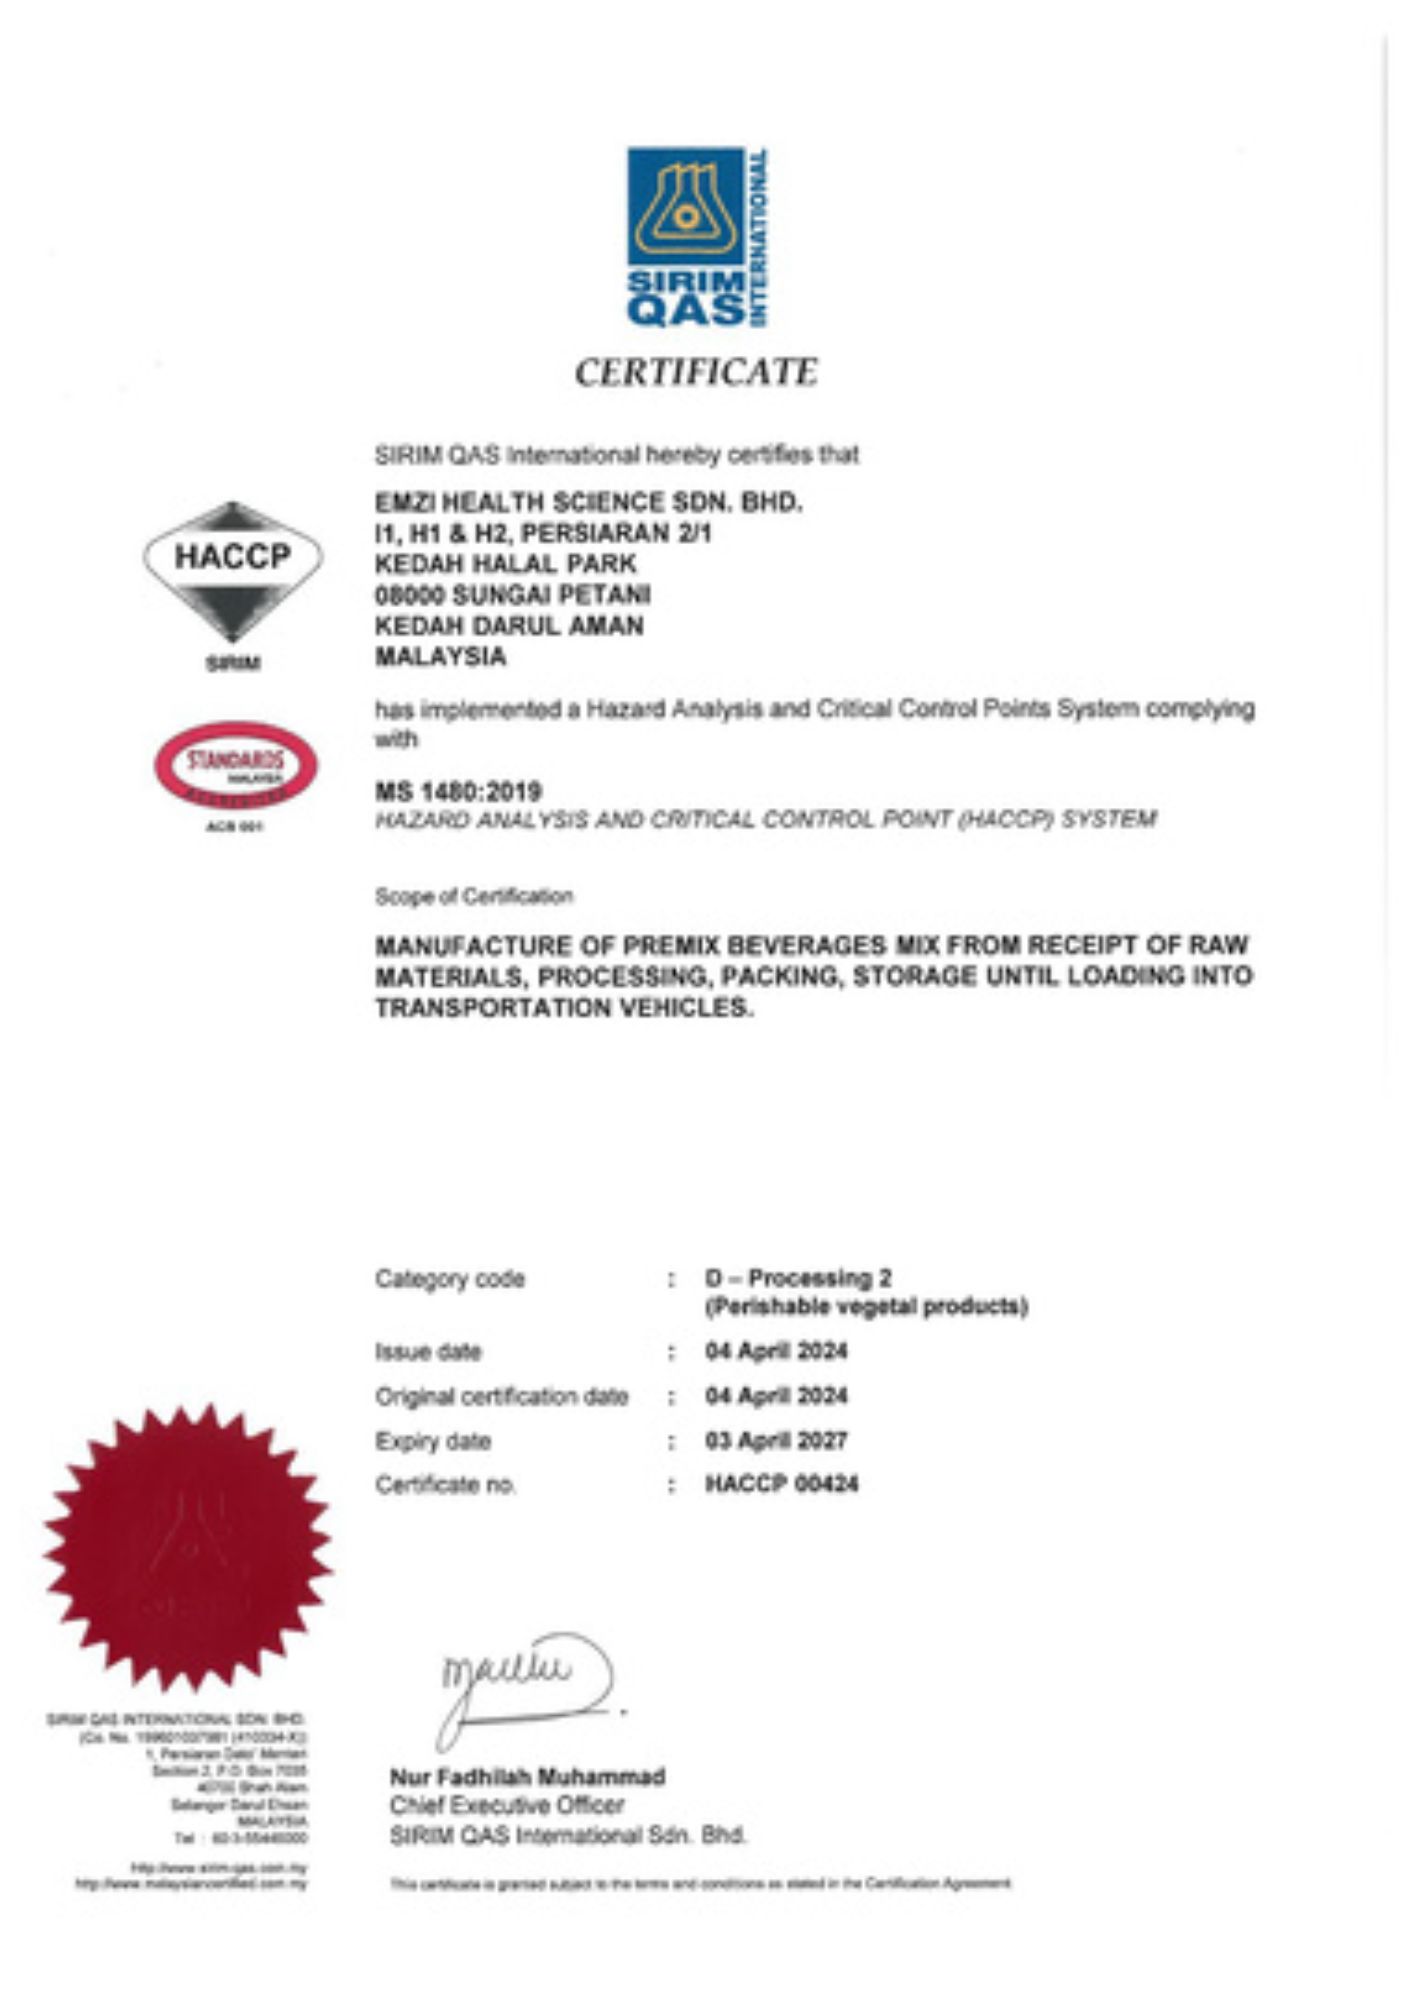
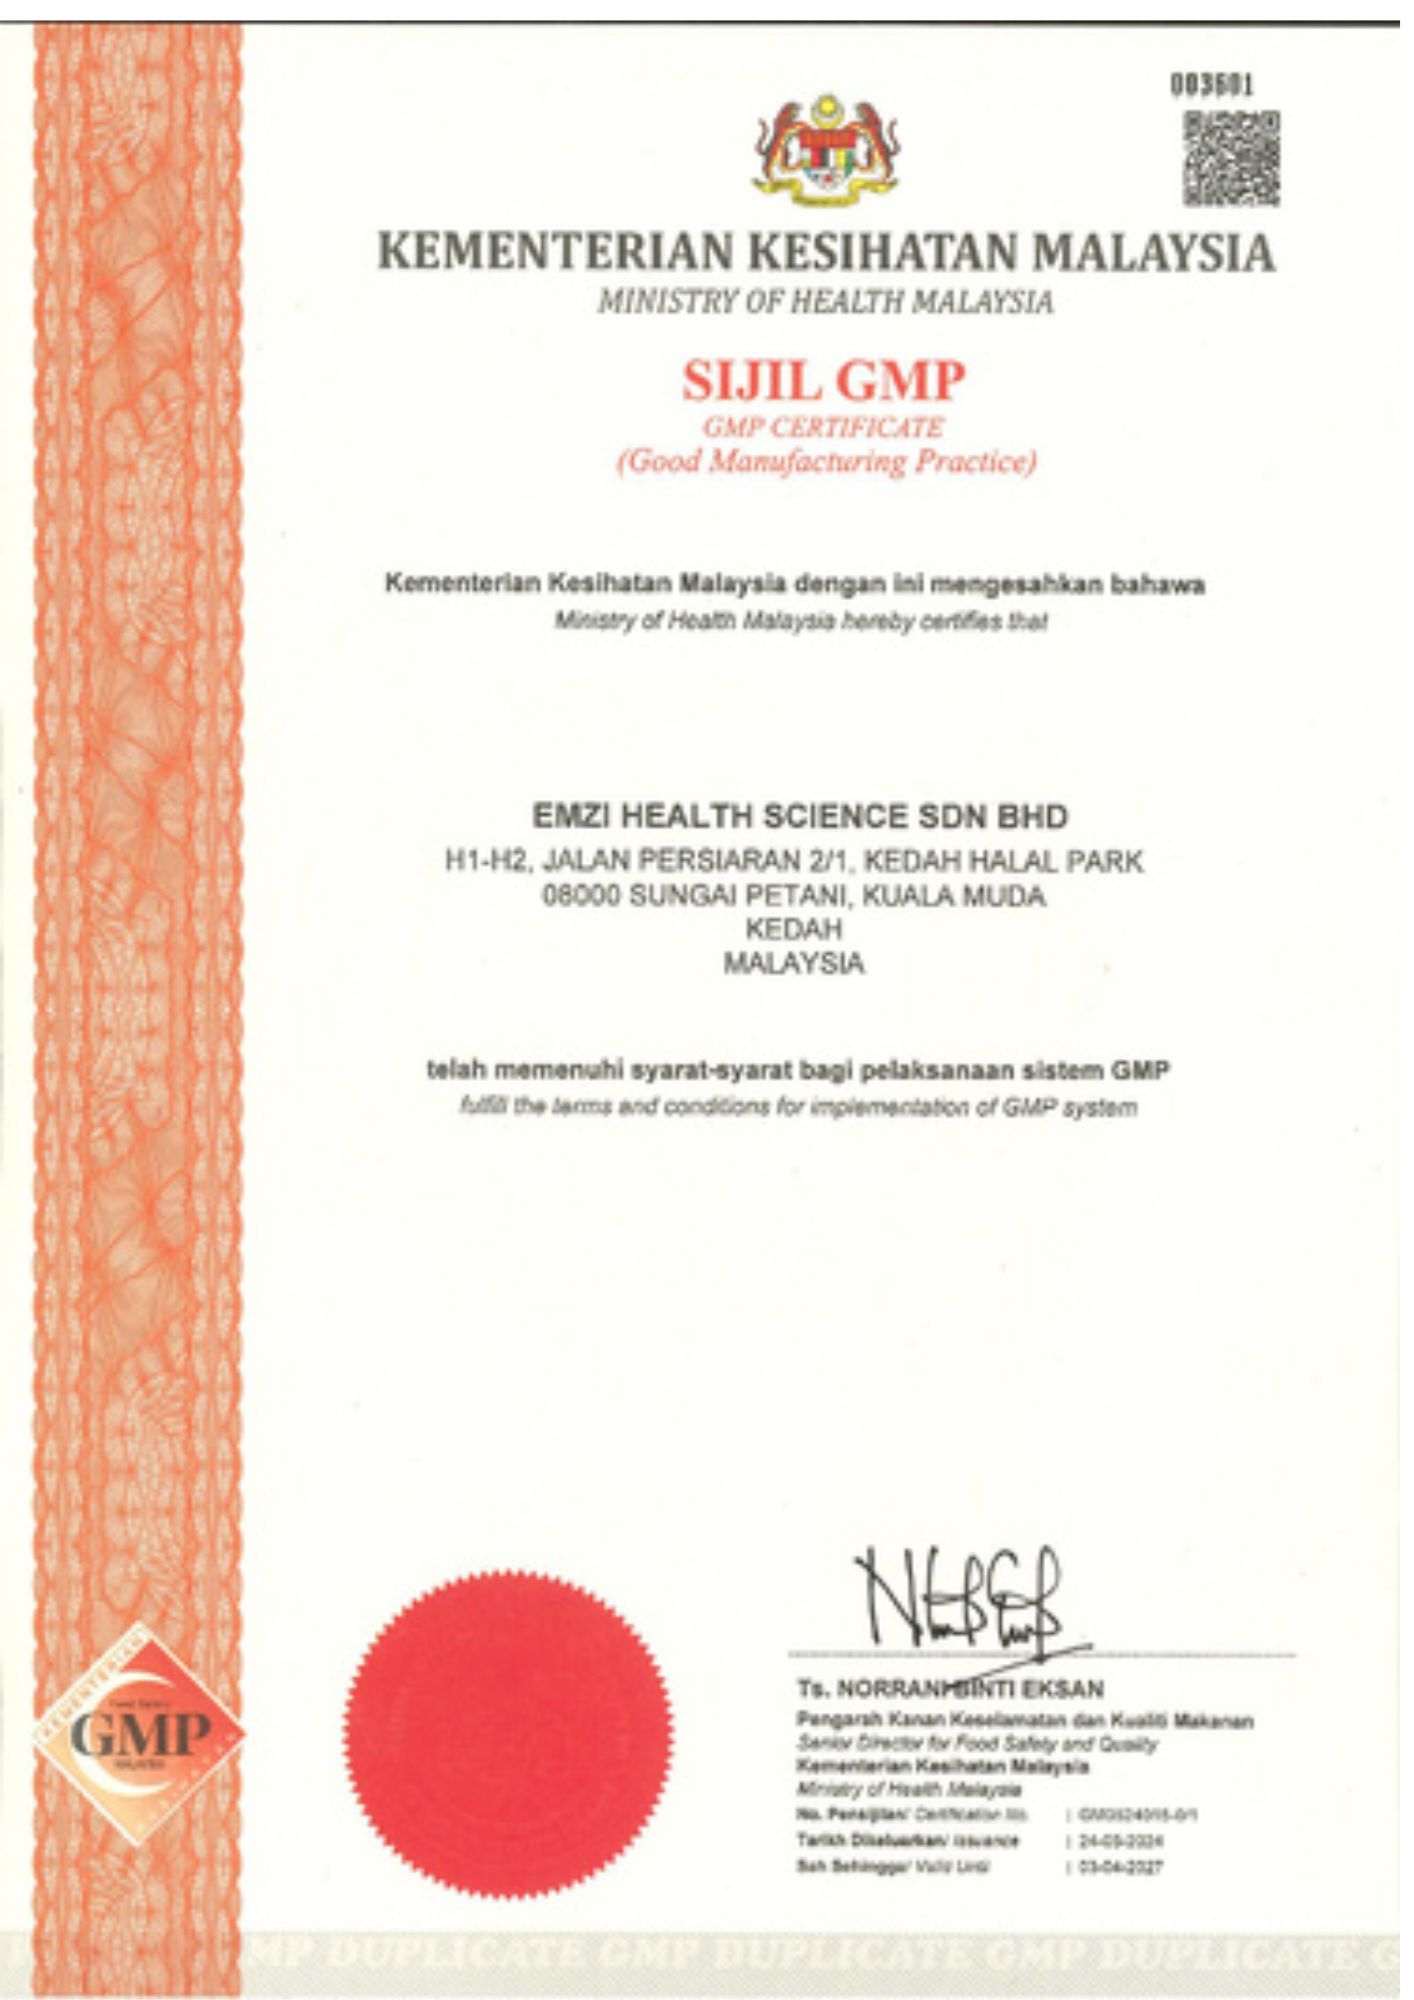
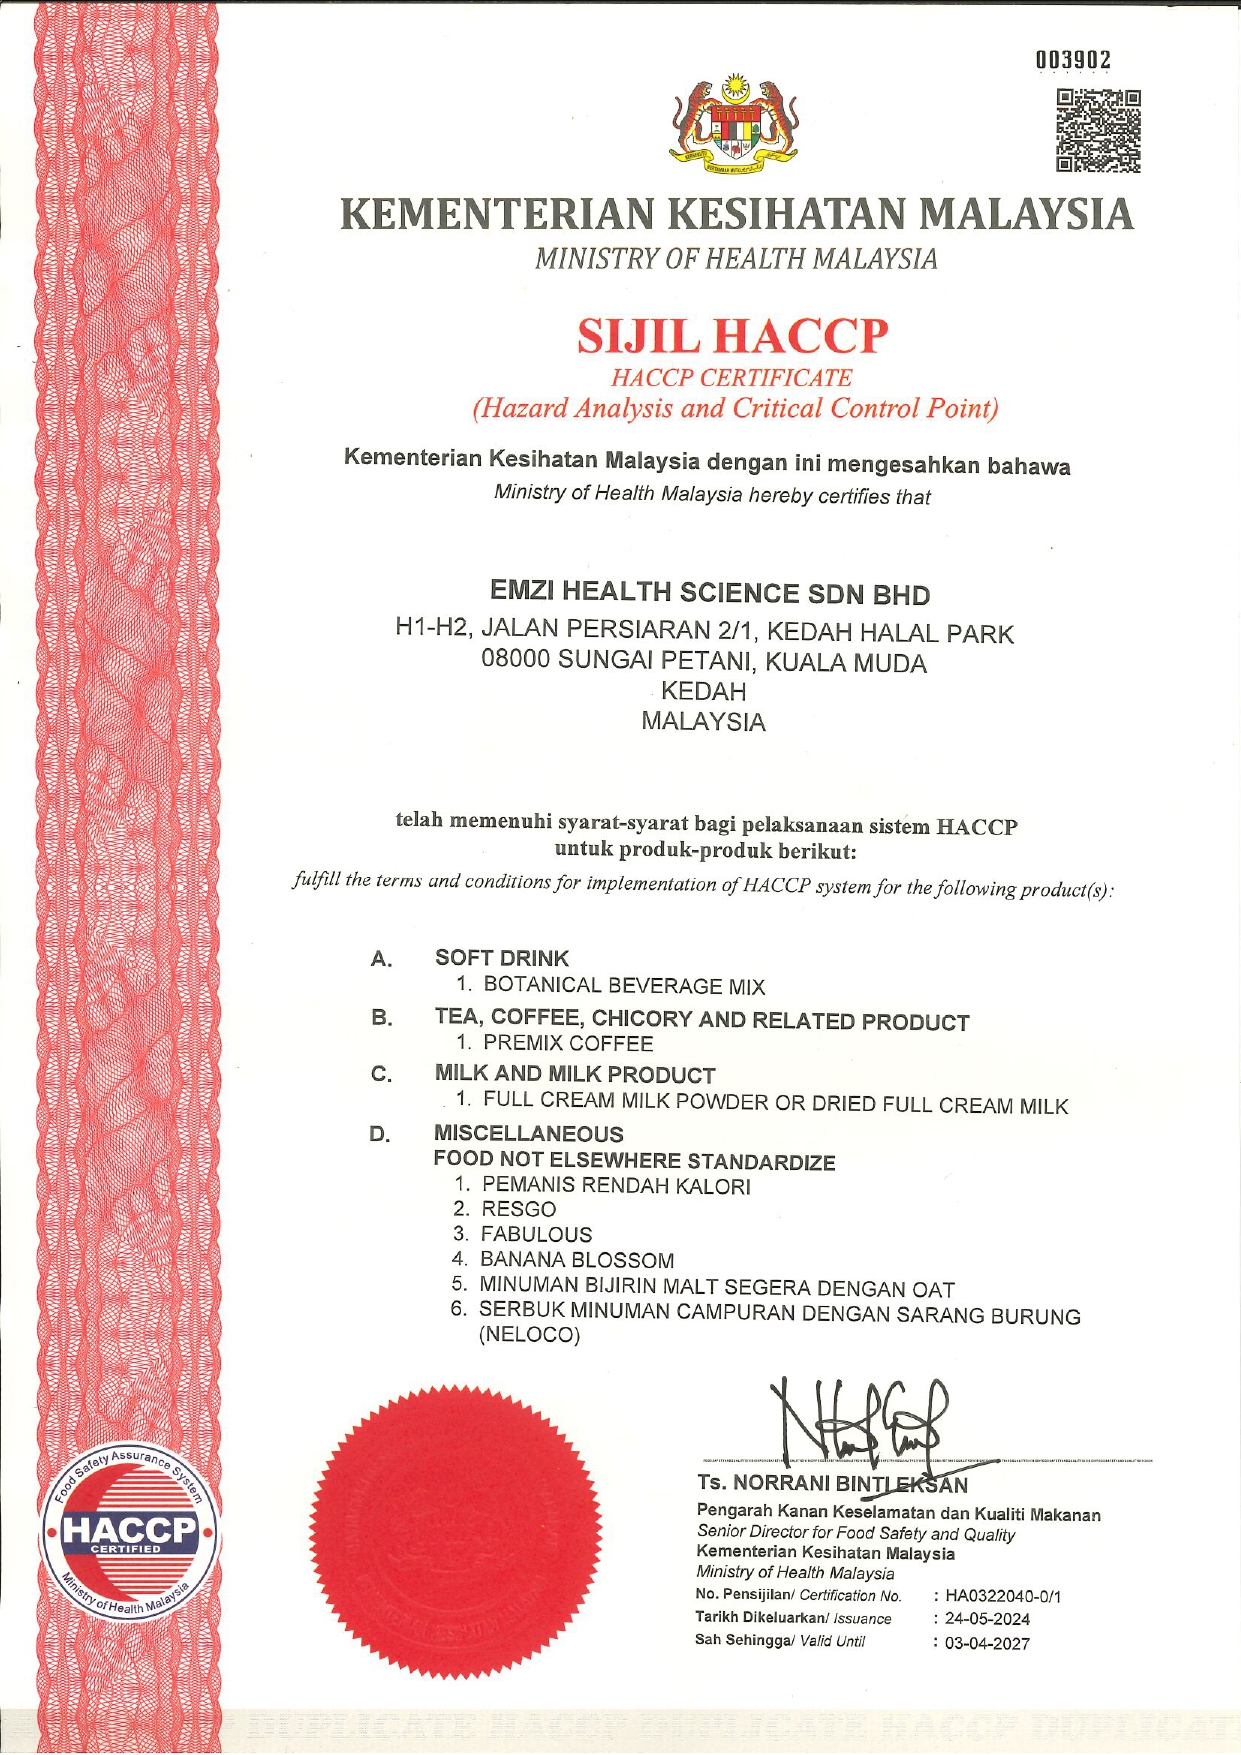
Our manufacturing operations are backed by HACCP, GMP, ISO 22000 Food Safety Management System and Halal Certification, demonstrating our commitment to food safety, product quality and regulatory compliance while supporting both local and international markets.
We are committed to improving the accessibility, convenience and effectiveness of healthcare products through strategic collaborations with local researchers and R&D institutions, driving innovation and advancing product development for better health and quality of life.
Our Specialties
Fully Automated Manufacturing System
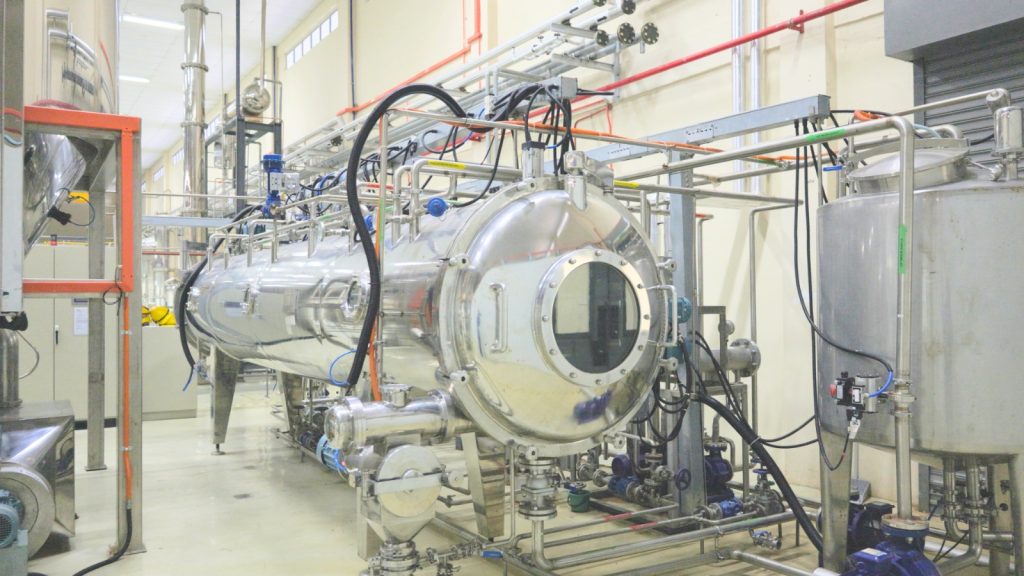
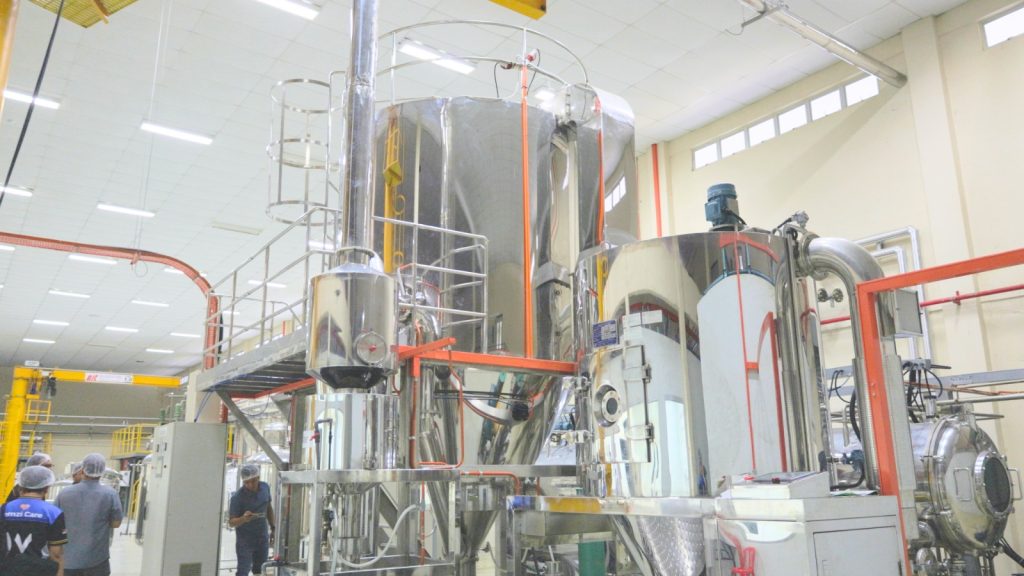
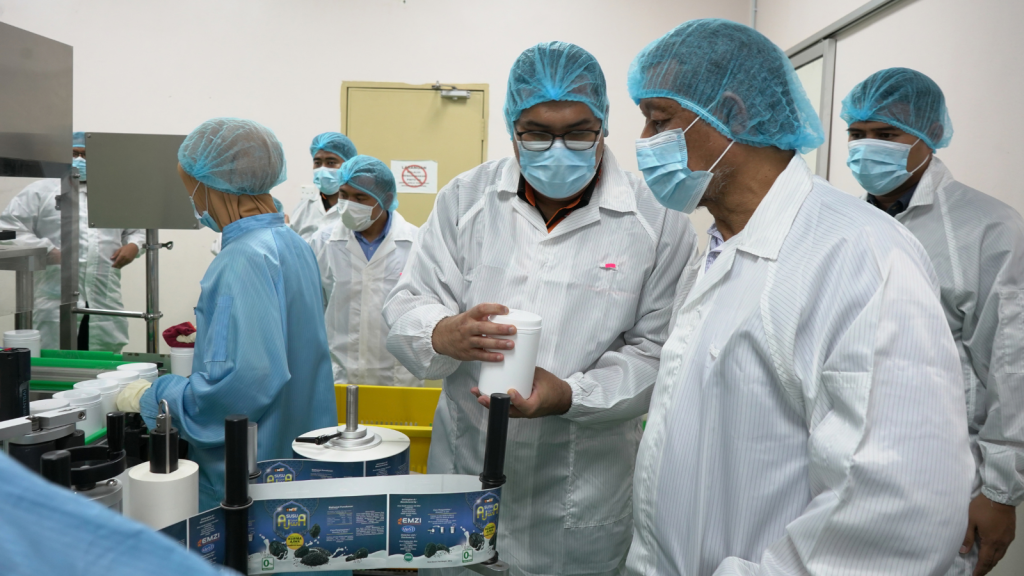
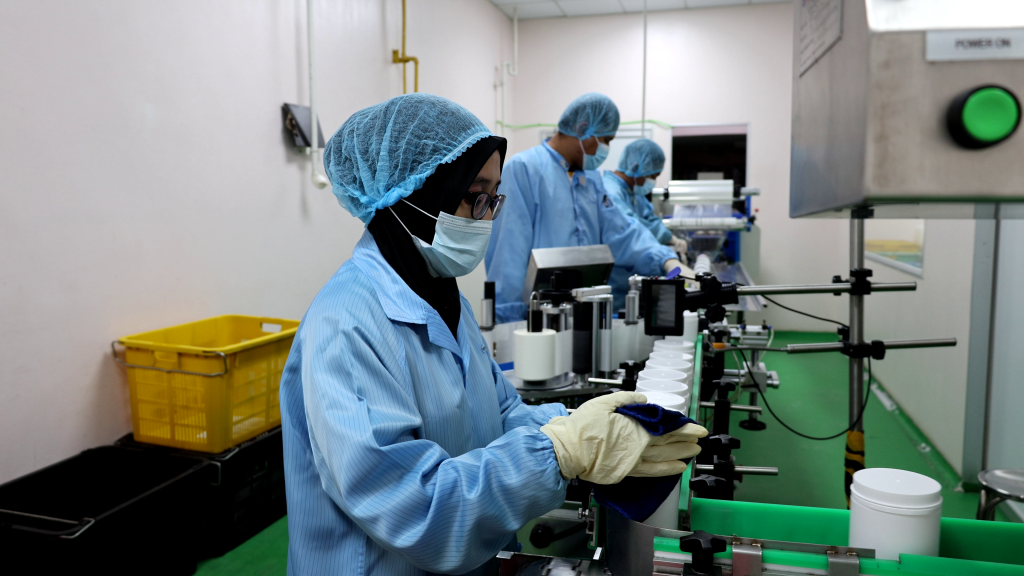
Our facility is equipped with fully automated and semi-automated machinery, enabling precise control across critical production stages such as raw material handling, blending, filling, sealing and packaging. This automation minimizes human error, enhances efficiency and ensures consistent product quality across every batch.
Dedicated Research & Development (R&D)
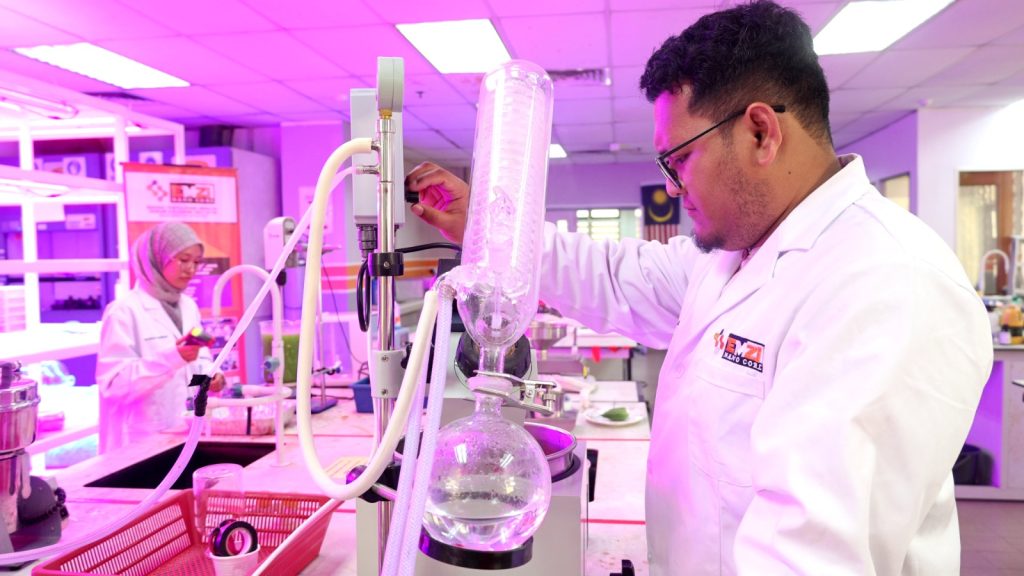
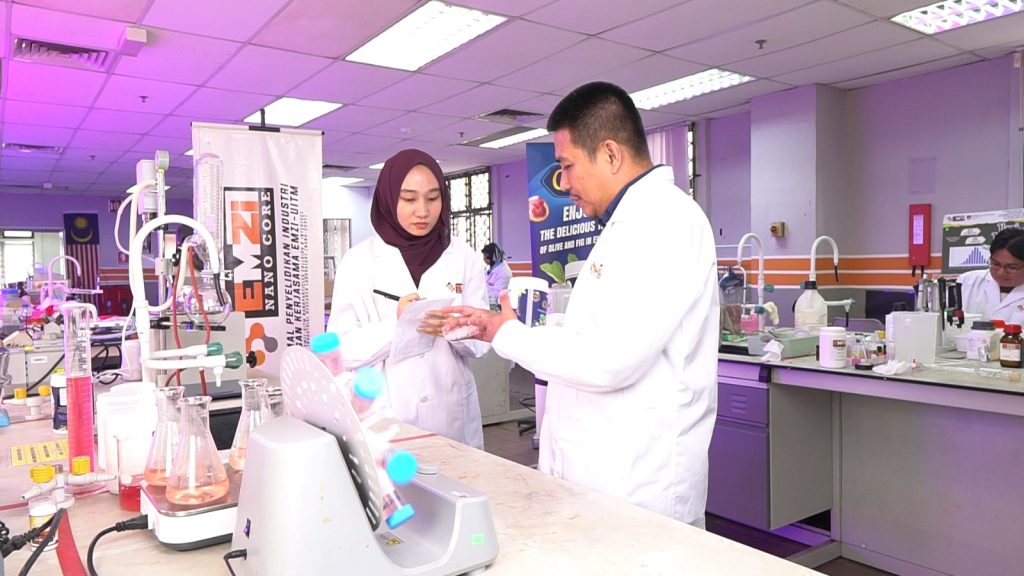
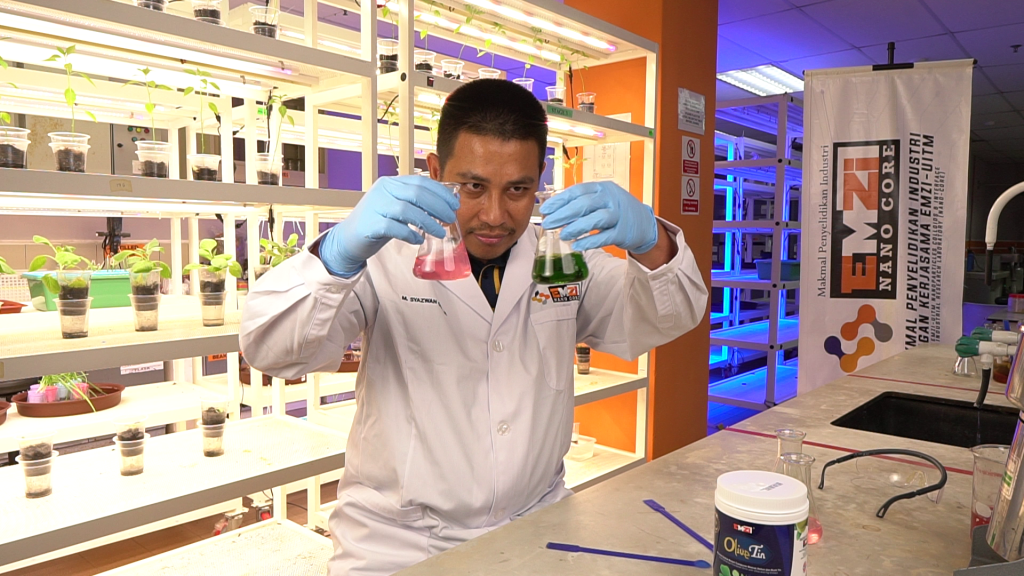
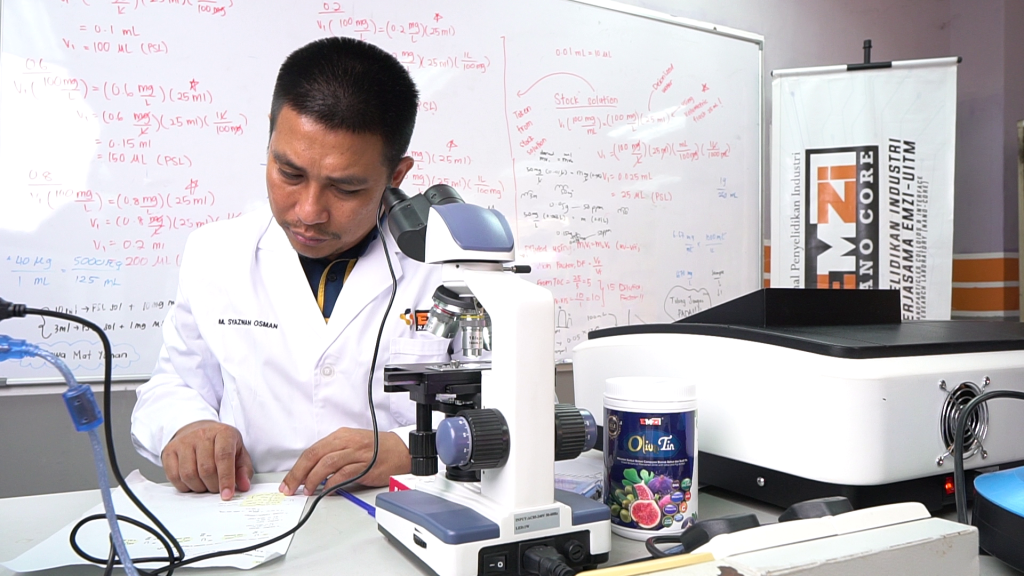
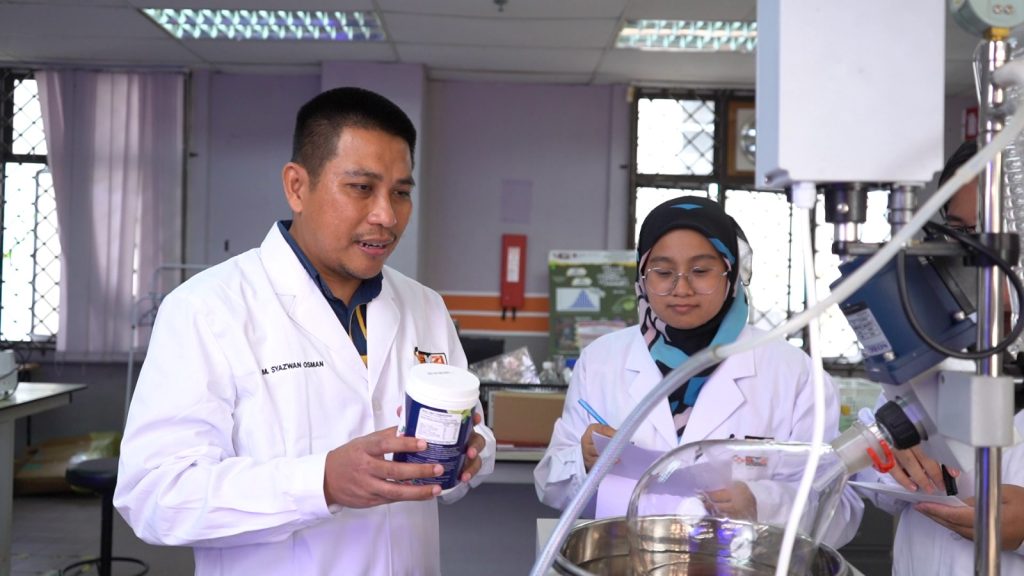
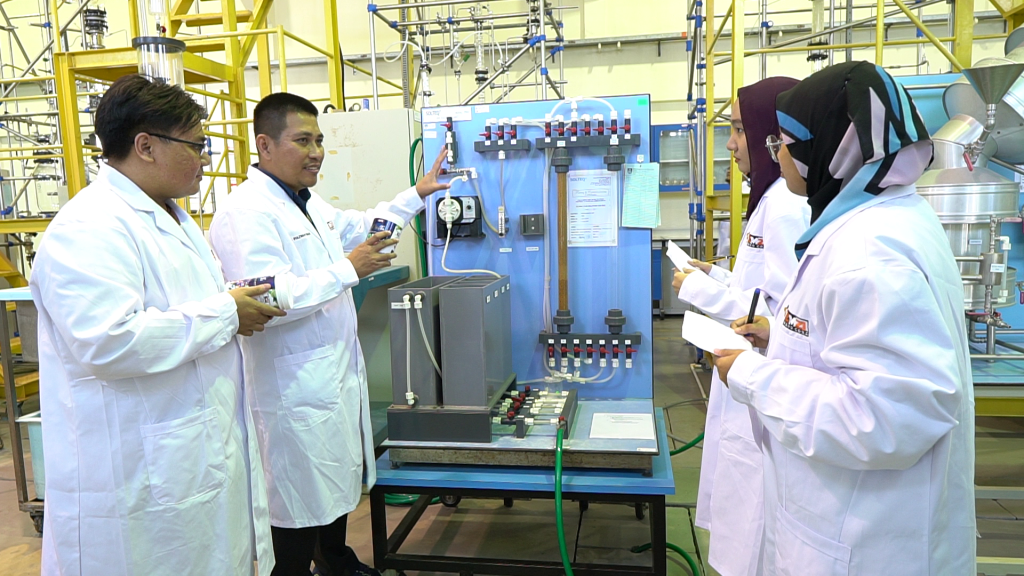
EMZI Health Science is supported by a dedicated Research & Development (R&D) team responsible for product formulation, innovation and continuous improvement. Our R&D efforts focus on developing functional, safe and effective health products aligned with scientific research and evolving consumer needs.
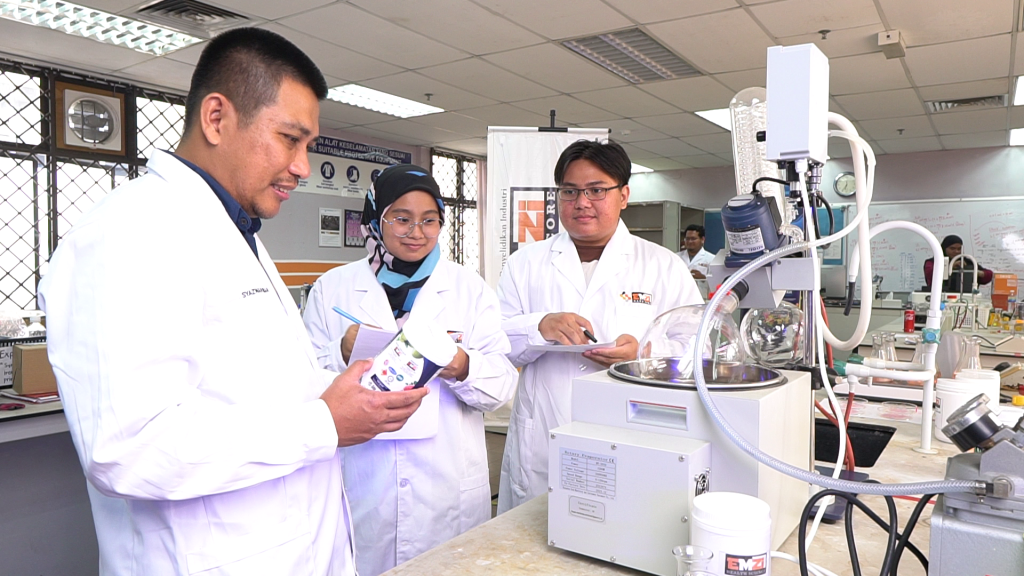
We actively collaborate with local universities and research institutions for formulation development, laboratory testing, validation and applied research. These collaborations strengthen our scientific foundation and ensure our products are developed using evidence based methodologies.
Quality, Safety & Process Control
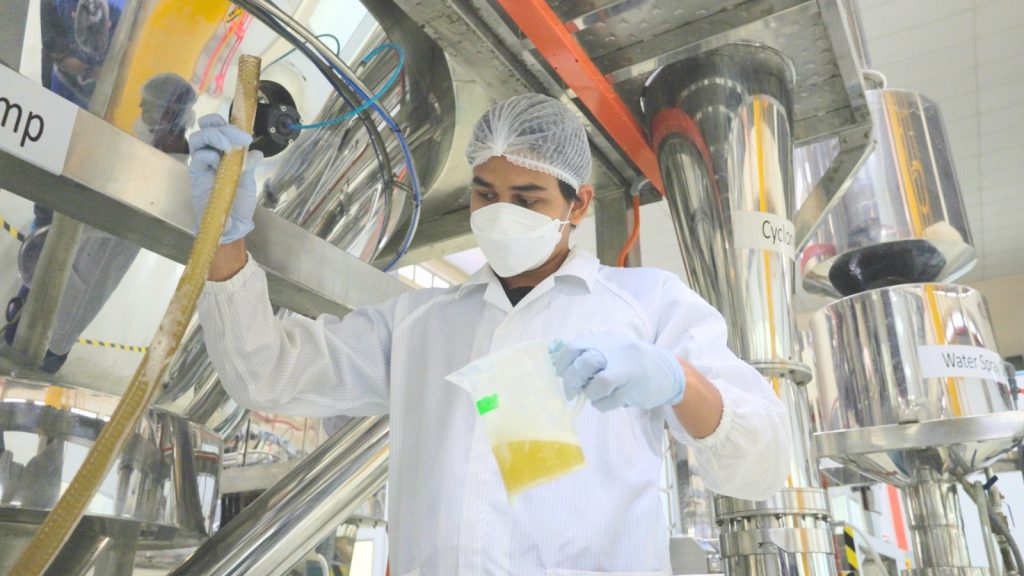
All production stages are governed by structured Quality Control (QC) and Quality Assurance (QA) systems. Raw materials are subjected to stringent inspection prior to use, while in process monitoring and finished product testing ensure compliance with safety, formulation and labelling requirements.
Regular internal audits, system validation and continuous improvement initiatives are conducted to maintain certification standards and operational excellence.
Halal-Compliant & Ethical Manufacturing
Our facility adheres strictly to Halal compliant manufacturing practices, ensuring ingredient traceability, proper material segregation and controlled handling procedures in line with recognized Halal standards and regulatory requirements.
Dedicated Fulfillment Centre
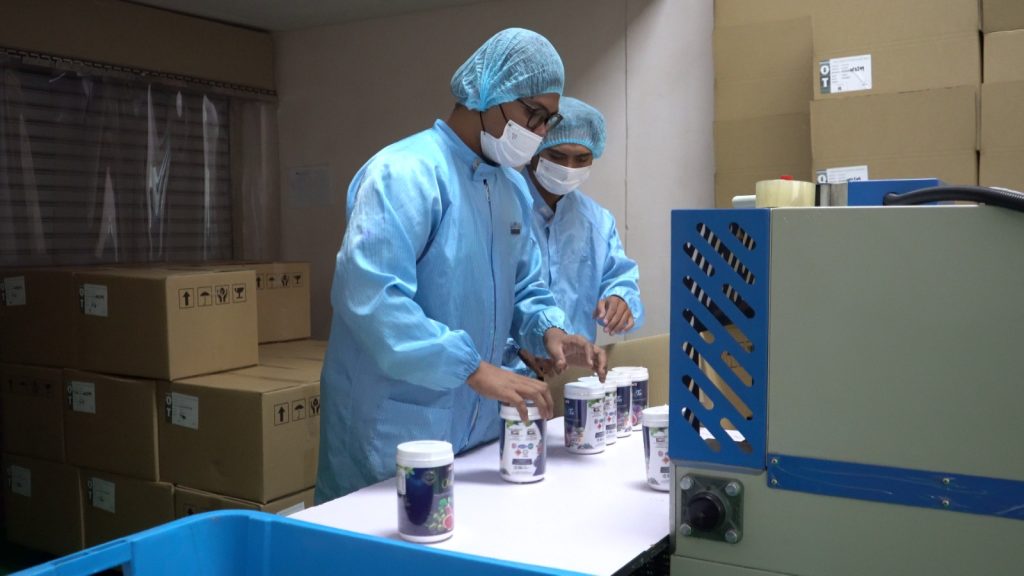
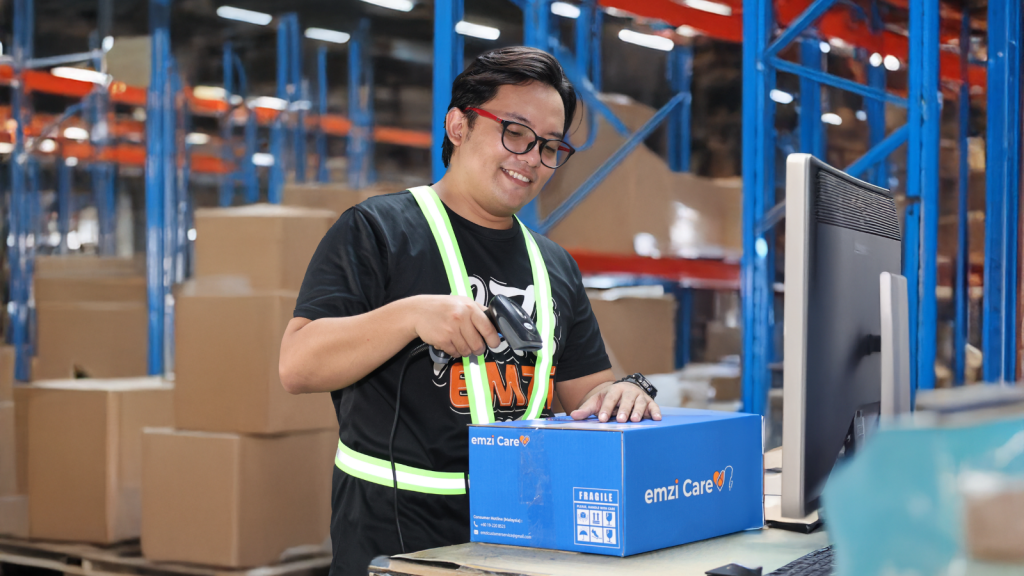
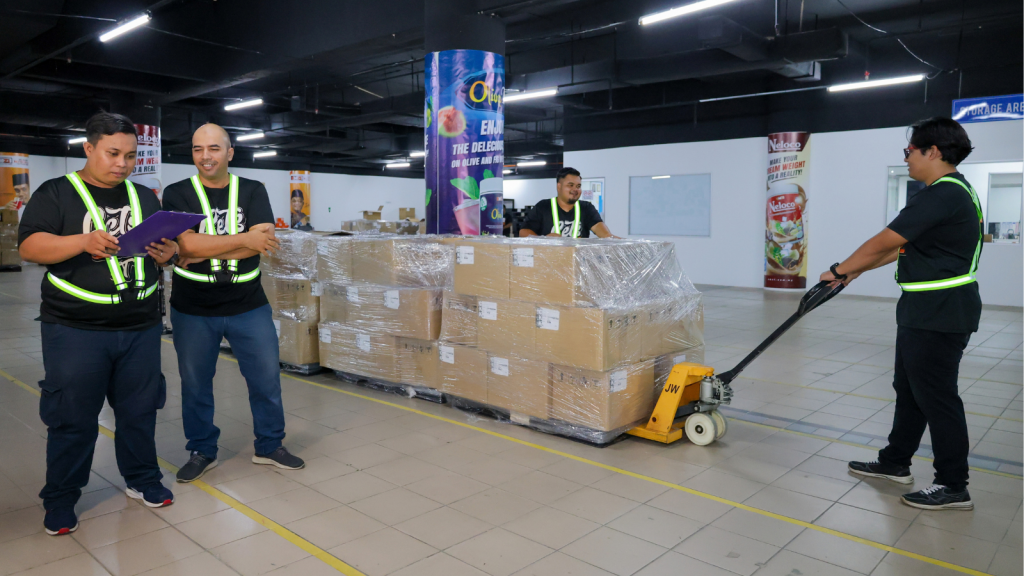
Complementing our manufacturing operations, EMZI Health Science operates a dedicated fulfilment centre designed to support efficient order processing, inventory management and nationwide distribution. The fulfilment centre is equipped with structured workflows, traceability systems and quality checks to ensure products are stored, packed and dispatched accurately and safely.
This integrated fulfilment capability enables us to support high volume e-commerce operations, wholesale distribution and export ready logistics with consistent service quality.
Build for Global Markets
Our manufacturing and fulfilment infrastructure is designed for scalability and international expansion, enabling EMZI Health Science to serve regional and global markets while maintaining consistent product quality, regulatory compliance and operational reliability.